


Imbalance in printing ink and rising defect rates
When our company uses the Heidelberg CD102 press for four-color printing, we found significant abnormalities in the magenta plate at 50% and 75% halftone in the text area (Figure 1). The main issues were unevenly enlarged dots, blurred images and text, noticeable color variations during printing, and a significant increase in the machine's water consumption. These problems caused obvious color fading, decreased saturation, loss of midtone gradation in the printed materials, and a noticeable increase in scrap rate.
Cause of the Fault
The staff first checked the impression cylinder and feed grippers and confirmed that lubrication was normal and the gripper pads were clean and free of debris. However, when inspecting the blanket cylinder inking roller pressure, unstable pressure was found. After a systematic inspection, the root cause of the fault was determined to be: the 80mm diameter operating side inking roller bearing seized due to a lack of lubrication, causing the bearing to lock. During machine operation, the bearing sleeve rotated synchronously with the inking roller, resulting in severe wear of the bearing cup (Figure 2). The amount of wear exceeded the standard range, leading to deep wear on the bearing seat mating surface.
When the machine is running idle, the 80mm diameter inking roller can move relatively smoothly within the bearing cup. However, during printing with pressure, the inking roller first comes into unilateral contact with the ink distribution roller, and after the pressure is applied, it contacts both the ink distribution roller and the printing plate simultaneously. Each rotation of the machine causes the inking roller to experience irregular wobbling in the worn bearing cup when it contacts the printing plate. This first damages the print dots, resulting in the blurred and deformed dot problem observed in Figure 1. In addition, the wobbling of the inking roller when in contact with the printing plate also causes irregular changes in the pressure between the inking roller and the ink distribution roller as well as between the inking roller and the printing plate, which can subsequently lead to ink streaking during printing and cause water-ink imbalance.
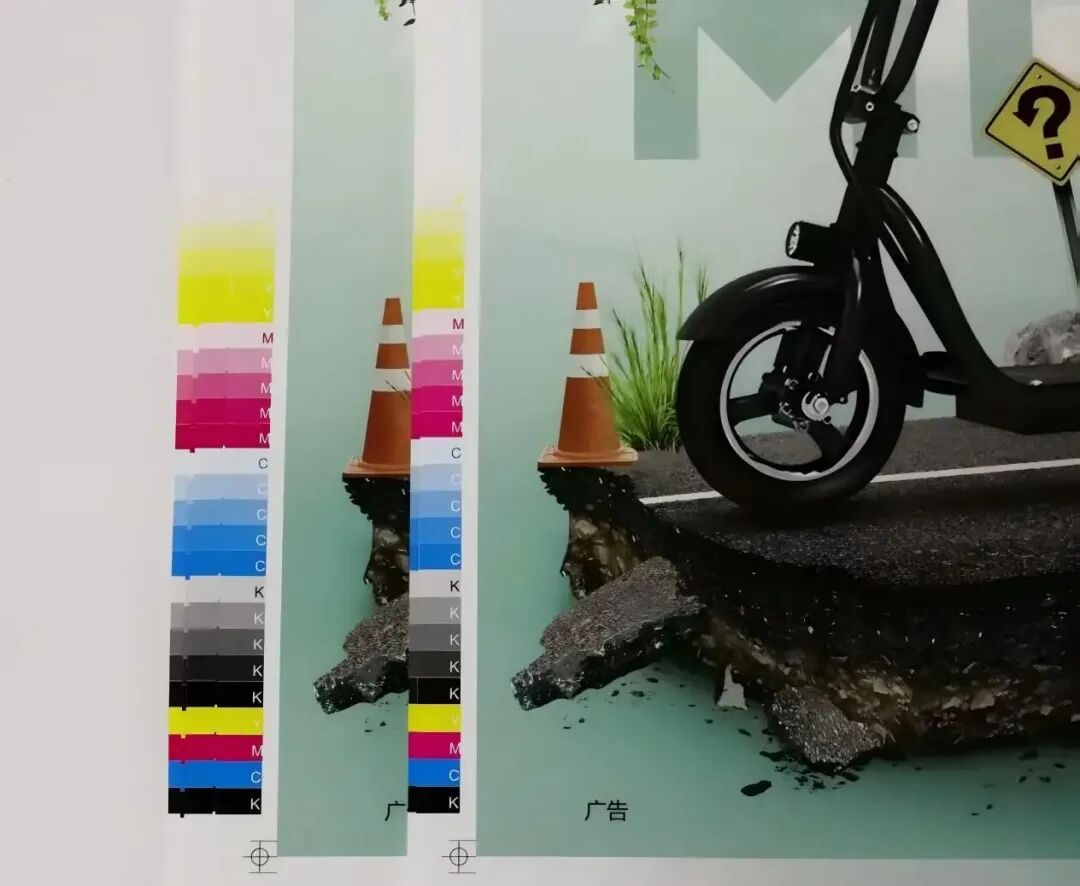
Figure 1 Problematic stamp (left) and adjusted stamp (right)
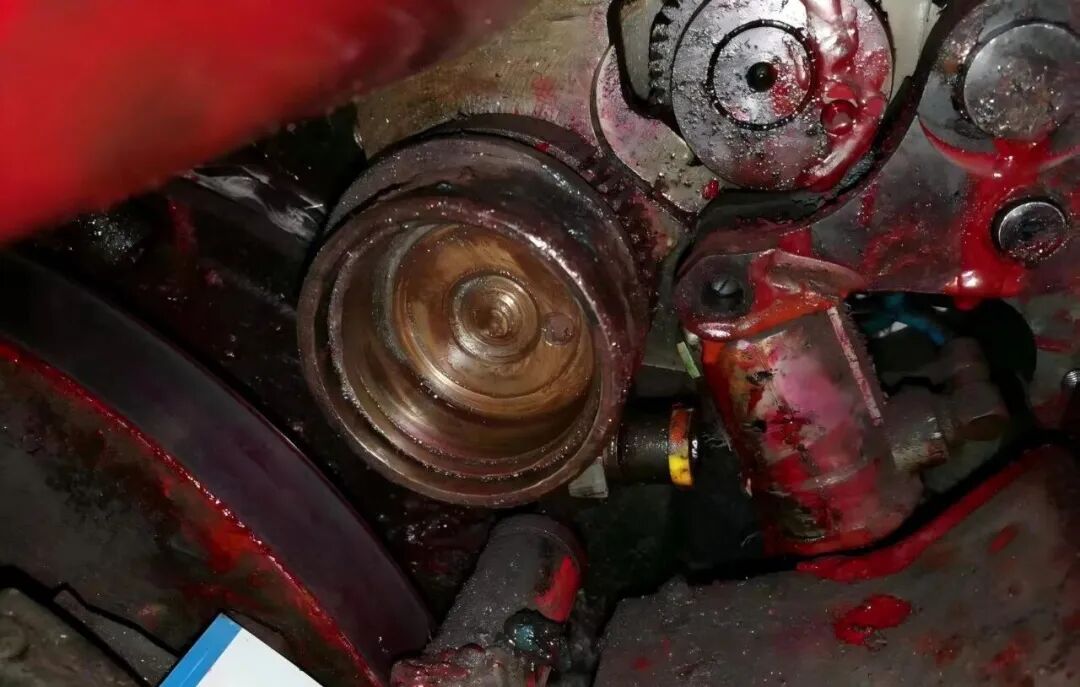 Figure 2 Wear Condition of the Anilox Roller Bowl
Standardized Maintenance Process
Since the form roller mainly relies on the fountain roller for movement and only performs a rhythmic slight deceleration when in contact with the printing plate, it is crucial to strictly follow the standard shown in Figure 3 when adjusting the printing pressure. The pressure ratio between the form roller and the fountain roller should be 1mm greater than the pressure on the printing plate. If the pressure between the form roller and the printing plate exceeds that between the form roller and the distributor roller, the form roller will decelerate irregularly, causing uneven ink transfer, excessive water and ink issues, and ultimately resulting in unstable ink color.
In actual production, when staff check the pressure of the form roller during daily inspections, they usually only pay attention to the pressure between the form roller and the printing plate, neglecting the pressure between the form roller and the distributor roller. The following is the standardized maintenance process:
(1) Shutdown and Cleaning: Disconnect power and post a lockout tag, then thoroughly remove the ink film on the roller surface and any metal debris inside the bearing housing using a dedicated cleaning agent.
(2) Component Replacement: Replace the original manufacturer's bearing assembly (including bearing bowl, balls, and cage). Before installation, perform ultrasonic cleaning and nitrogen blowing to ensure a contamination-free assembly.
(3) Pressure Calibration: Use Heidelberg pressure test film for calibration (as shown in Figure 3).
(4) Define Pressure Standards: The ink mark width between the form roller and fountain roller should be 4 ± 1mm; the contact width with the printing plate should be set to 4–1mm.
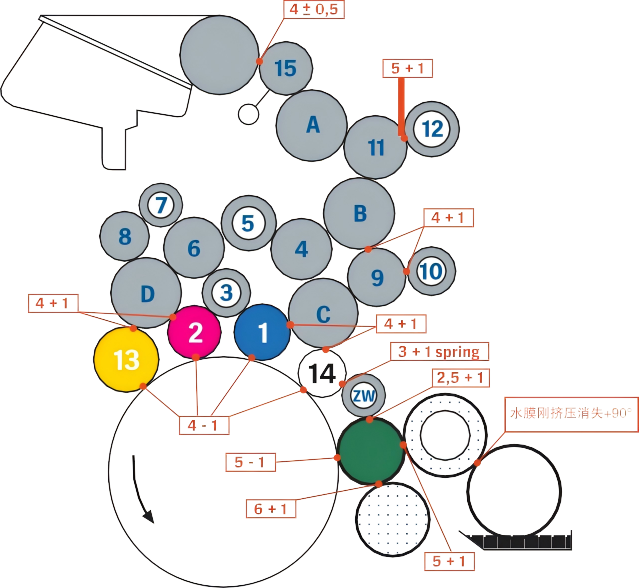
Figure 3 Printing Pressure Adjustment Standard
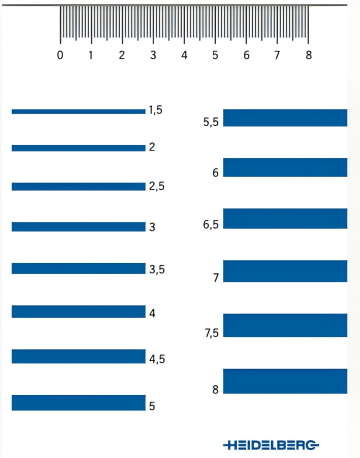 Figure 4 Heidelberg stress test film
Maintenance effect
After standardized maintenance, the quality of equipment and printed products has been significantly improved, and all indicators have returned to the normal range:
(1) The 50% outlet increase value of the magenta version fluctuates back and forth from 22%~45% before maintenance to about 18% (in line with the requirements of 17±3% outlet increase).
(2) The gradient smoothness of the gradient level of 75% dot density is increased by 40%, and there is no obvious discoloration during the printing process.
(3) The data monitoring of continuous production for 8 hours shows that the printing water consumption (after the repair of the faulty unit) is reduced by 20%, and the scrap rate is reduced from 22% to 0.2%.
(4) The equipment stability monitoring found that during 72 hours of continuous operation, the infrared thermal imager showed that the temperature of the plate roller bearing was stable in the normal range of 40±2°C, and there was no abnormal peak in the vibration spectrum analysis.
Problem analysis
01/ Defects in maintenance mechanisms
One of the core causes of this failure is that there are obvious defects in the equipment maintenance mechanism, and the relevant operations violate the requirements of the equipment maintenance manual, which stipulates that the ink roller needs to be disassembled every month, the bearing condition should be checked, lubricating oil added and the ink roller pressure should be adjusted in a standardized manner. In addition, during the previous maintenance, ordinary feeler gauges were mistakenly used instead of Heidelberg's special ink trace width detection film, resulting in a gap setting deviation of 2.2mm, and the pressure of the ink roller was mistakenly set to 6.2mm (55% exceeding the standard value), resulting in bearing overload.
When the normal indentation of the rubber roller is 4mm, the pressure is 18N; When the indentation reaches 6mm, the pressure increases to 63.5N, and when the indentation reaches 8mm, the pressure is as high as 149N. The larger the indentation, the faster the wear of the equipment, the higher the consumption of ink and dampening fluid, and the corresponding increase in electricity consumption. At the same time, excessive pressure will lead to obvious heat accumulation of the rubber roller, higher temperature and wide indentation, which will increase the actual pressure in the printing process nonlinearly, accelerating the hardening of the rubber roller. Although the hardness of the rubber roller can enhance the corrosion resistance to a certain extent, it will significantly reduce the water and ink transfer capacity, increase the ink loss of the printing equipment and the wear of the printing plate graphics. Therefore, without affecting the printing quality, the pressure of the rubber roller should be reduced as much as possible, and the minimum value specified by the manufacturer should be kept as optimal.
02/ Do a good job of rubber roller maintenance
The daily maintenance of rubber rollers needs to form a standardized process, and the pressure of the plate needs to be checked during the daily handover; During weekly maintenance, it is necessary to focus on checking the pressure of the plate roller and the ink roller, and do a good job in the maintenance of the plate ink roller to ensure that it is always maintained in a relatively stable state during production.
The surface of the new rubber roller should be uneven, and it feels a little astringent to the touch (Figure 5), so as to ensure the uniform transfer of water film and ink. In the process of long-term use, due to the constant contact with ink, dampening fluid and various solvents every day, coupled with the influence of the external environment, the hardness of the new rubber roller will usually increase after a period of use, which is a normal state. If the shrinkage and hardening of the rubber roller are light, the ink transfer characteristics can be maintained by adjusting the pressure appropriately.
The increase of the hardness of the rubber roller also means that the paper wool paper powder and the oxidized substances in the dampening solution have been deposited on the surface of the roller, forming a hardened film. This hardened film must be removed periodically (Figure 5) to prevent it from continuing to harden and glaze, which can cause instability in ink transfer and water transfer. When the surface hardens, the dirty glazing substance should be removed with calcium removal paste during maintenance.
The choice of cleaning agent is the most critical factor in determining the life of the rubber roller. Although highly volatile detergents are easy to remove hardened sediments on the surface, they will also cause the shrinkage of the rubber rollers. Improper use of cleaning agents will also lead to the expansion, contraction and deformation of the rubber rollers, affect the stability of the pressure between the rubber rollers, and even corrode the pipelines, sealing rings, machine paint and even rubber blankets. Therefore, semi-water-based, low-VOCs car wash water should be chosen. After maintenance, the rubber roller needs to be restored to the feel of the new rubber roller to be considered in place. There are no shortcuts to maintenance, and it must be persistent.
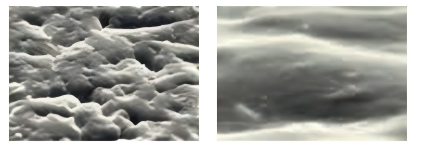
Figure 5 Surface of a new rubber roller (left) and surface of the rubber roller after glazing (right)
The key to print quality lies in ink-water balance, and the fountain roller and ink roller play a crucial role in maintaining this balance. In daily production, various quality issues caused by improper roller adjustment or roller wear are common. Therefore, it is essential to regularly inspect and check the rollers during work, and to maintain and adjust the roller surface, diameter, and pressure periodically to ensure that each roller is in proper condition. Equipment adjustment should be data-driven and standardized, contributing to the high-quality development of the industry.