


High Scrap Rate in Cigarette Pack Hot Stamping, Improving This Device Can Effectively Reduce It!
Currently, in the cigarette pack products at the company I work for, during the 3D hot stamping process, we often have to stop the machine because the pressure is either too high or too low. We pull out the stamping base repeatedly to adjust the pressure, and finding the exact spot that needs pressure adjustment and how to adjust it takes some time, which leads to hot stamping scrap. Additionally, since operators can't directly locate the areas that need pressure compensation, they have to repeatedly search and stop the machine to make adjustments. During this process, the stamping temperature changes, which also produces scrap, as shown in Figure 1. All these factors directly affect the production efficiency and yield of cigarette packs.
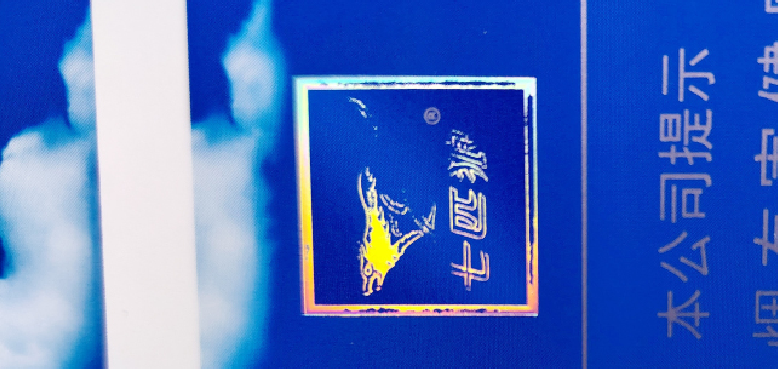
Figure 1 Hot Stamping Waste
Problems with Existing Methods
The current 3D hot stamping pressure compensation method mainly involves sticking the compensating pressure paper directly on the back of the resin die (① in Figure 2), and then using glue to attach it to the hot stamping base plate (②), thereby adjusting (increasing) the pressure during the hot stamping process. If the pressure does not meet the process requirements during stamping, the entire resin die needs to be lifted. Then, by comparing the stamping results with the product, the areas that need pressure adjustment are identified. After locating the corresponding spots, the pressure paper is stuck on the back of the resin die (①-2) and fixed to the hot stamping base plate (②) using glue, achieving pressure compensation.
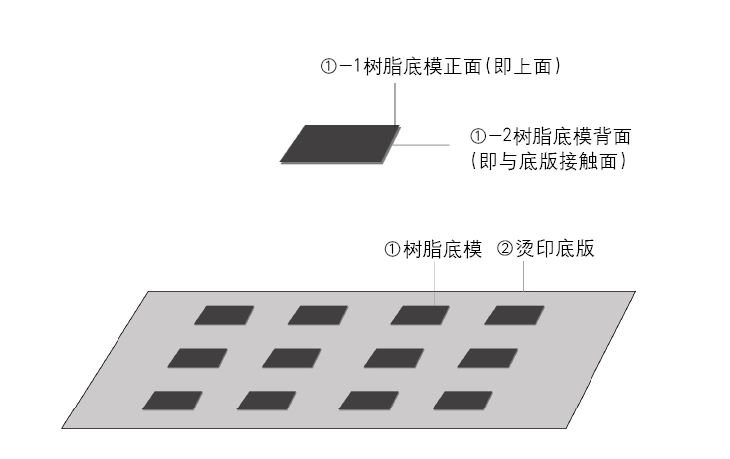
Figure 2: Schematic of the Original 3D Hot Stamping Compensation Pressure Device
During this process, the position of the resin base mold and the stamping die may change, so the position needs to be repeatedly checked and adjusted. This leads to long adjustment times and can easily result in defective stamps if the position is off. At the same time, because of the repeated adjustments, the base layer paper can deform or get damaged, which affects the overall stamping quality. The side view of the original 3D hot stamping compensation pressure device is shown in Figure 3.
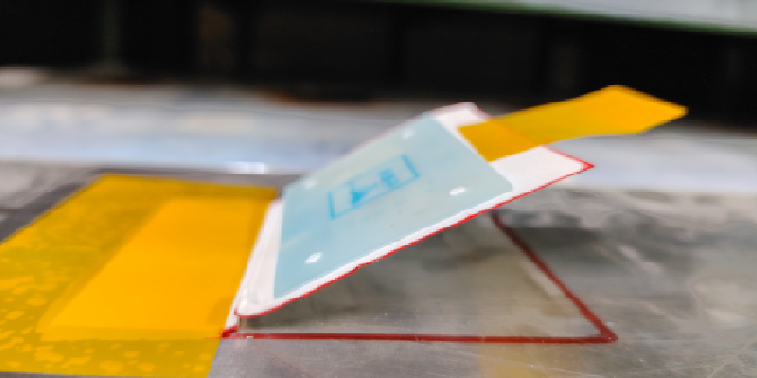 Figure 3 Side view of the original 3D hot stamping pressure compensation device
Additionally, due to differences in operators' skill levels, the timing and effect of 3D hot stamping pressure compensation can also vary.
Feasibility Analysis and Verification
During the use of the original positioning device, taking the "Seven Wolves (Blue)" cigarette pack small box as an example, the 18-piece product has a total of 36 hot stamping positioning devices. Adjusting the pressure generally takes 7–9 hours or even longer. Each adjustment can cause misalignment between the resin base mold and the hot stamping base plate, requiring repositioning and adjustment, which is time-consuming. At the same time, during the hot stamping process, the stamping pressure directly affects the stamping result. Too much or too little pressure can produce defective products, such as sand holes, incomplete stamping, or gold flying, which requires stopping the machine to check and adjust the pressure where needed. The stamping area usually occupies a small proportion of the total product area, so the adjustment area is small and changes greatly, requiring a lot of patience for repeated pressure adjustments. Frequent stops of the hot stamping machine directly affect the equipment temperature; temperatures that are too high or too low can lead to defective products, so the materials chosen for the device need to consider high-temperature resistance and stability, while also avoiding deformation or damage during repeated flexible adjustments and movement.
By analyzing the above issues, the project team optimized and upgraded based on the original resin materials and product performance. They plan to adopt a resin material positioning device that allows for quick pressure adjustment, using a composite structure for fixed positioning parts while making the core area movable or adjustable. This design allows the overall structure to have a fixed base and an embedded movable part, enabling 3D hot stamping pressure compensation during pressure adjustment, effectively shortening adjustment time and reducing machine-related waste.
Additionally, to address the issues of repeatedly adjusting pressure and finding the compensation area, the device needs to incorporate basic pattern lines of the hot stamping design. Considering these factors, the project team, in material selection, besides using a fixed resin base mold, also chose cardboard commonly used in cigarette packaging as the base for the fixed part (overall design is mainly trapezoidal to ensure connection between fixed and embedded structures). They also prepared a certain amount of translucent tracing paper (with the content to be stamped printed on it) and a copper sheet as a buffer layer, ultimately forming an embedded device for rapid 3D hot stamping pressure compensation. The exploded material diagram and actual application perspective are shown in Figures 4 and 5.
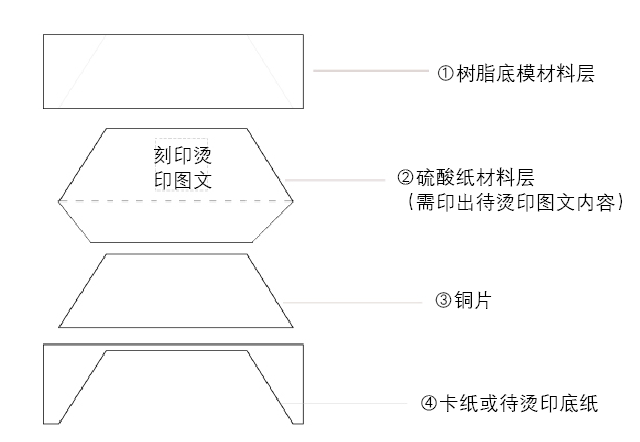
图4 嵌入式快速补偿立体烫印工艺压力装置的材料分解图
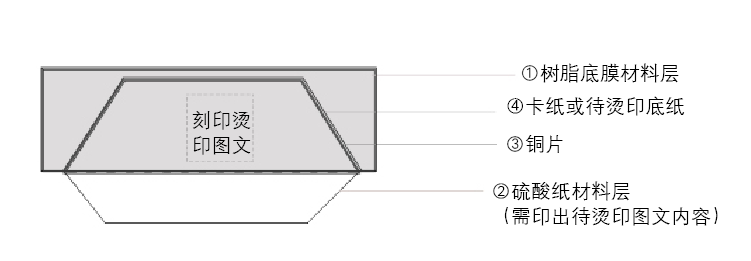 Figure 5 Perspective View of the Actual Application of the Embedded Rapid Compensation 3D Hot Stamping Pressure Device
In Figures 4 and 5, Material ①, the resin base mold layer, has an overall frame size consistent with ④ cardstock or the paper to be hot-stamped. Its main function is to ensure the first layer fully adheres and matches the base layer, protecting the embedded devices and material properties of ② and ③.
Material ②, the sulfur paper layer, is absorbent and can capture moisture generated by heat during the hot-stamping process while remaining deformation-free and undamaged. At the same time, the sulfur paper layer needs to be printed or drawn according to the pattern on the resin base mold. Depending on the display effect of the product's hot-stamping area, you can directly position the areas where pressure needs adjustment, reducing inspection and setup time, lowering defective rates, and improving production efficiency.
Material ③, the copper sheet, has a certain toughness and provides cushioning during the hot-stamping process, protecting the resin base mold from cracking and making it easier to remove and insert the sulfur paper layer.
Material ④, the cardstock or paper to be hot-stamped, is designed with openings; the open areas correspond to the appearance areas of ② and ③. Together, ④ forms a complete embedded slot design that keeps materials in place without shifting or deforming. The overall material of ④ fits the hot-stamping process requirements better. This layer is fixed after alignment with the hot-stamping plate and is not moved during subsequent pressure adjustments, making it directly attachable to the stamping base.
Performance of the Improved Design
The improved positioning device first addresses the issue of repeated checks and misalignment caused by lifting the entire resin base in the original pressure compensation method, reducing hot-stamping waste due to misalignment. Secondly, the embedded structure ensures overall alignment stability while allowing the copper sheet and sulfur paper to be pulled out for pressure compensation at the corresponding positions, reducing the time needed for adjustment and finding pressure areas. Moreover, the embedded design, together with material selection, minimizes issues with remaking the pressure device due to moisture absorption, thereby improving device utilization.
Figure 6 shows the disassembly of the embedded rapid compensation 3D hot-stamping pressure device, with specific functions as follows: using an embedded approach, different material layers are flexibly pulled (pull-out schematic shown in Figure 7) according to adjustment needs. The composite structure of the sulfur paper layer (with printed graphics) and copper sheet can be pulled out for corresponding adjustments, allowing easy and repeatable operation. Figure 8 shows a schematic of the assembled embedded rapid compensation 3D hot-stamping pressure device.
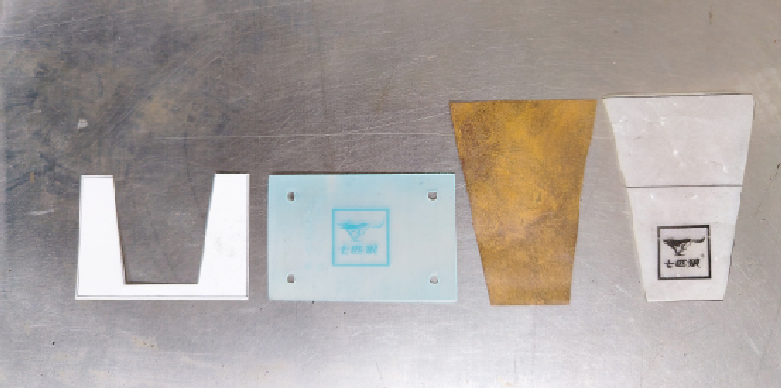
Figure 6: Disassembly diagram of the pressure device for the embedded rapid compensation 3D stamping process
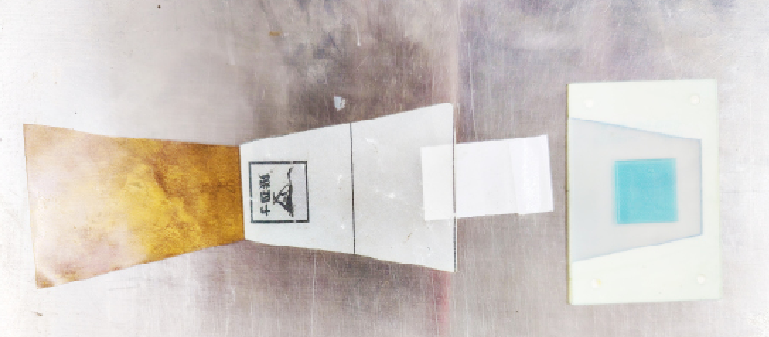
Figure 7 Pull-out Section Expanded View
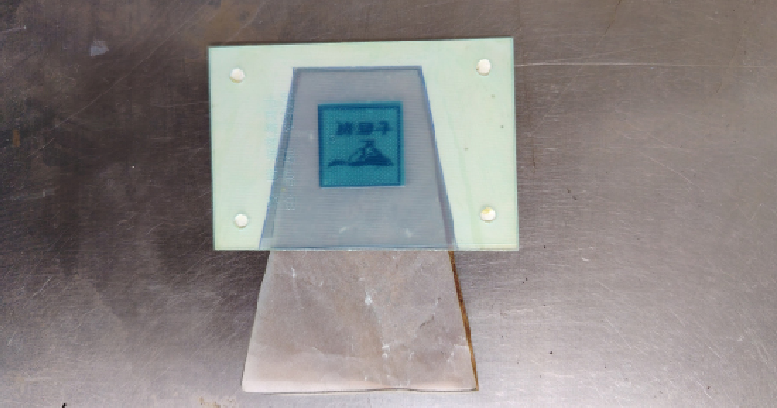
Figure 8: Schematic Diagram of the Embedded Rapid Compensation Stereoscopic Hot Stamping Pressure Device
In actual production, the resin base film layer and the cardstock part form a fixed trapezoidal area. When pulling the composite structure of the sulfuric acid paper and copper sheet, the pressure compensation on the sulfuric acid paper can be adjusted according to the quality of the product's stamping area. Material characteristics such as the water absorption of the sulfuric acid paper and the toughness of the copper sheet make them less prone to deformation or damage during repeated pulling, protecting the resin base mold from cracking while maximizing the stability of the overall stamping device. Additionally, the fixed trapezoidal area ensures the device stays accurately positioned and doesn't shift easily.
After running steadily for a period, the new positioning device (as shown in Figure 9) has been applied in the production of the company's 'Seven Wolves (Blue)' small cigarette packs. The device performs very well, with pressure adjustment time stabilized at 2–3 hours. Compared to before, this is about a 71.43% reduction in time, meeting the expected goals and improving efficiency.
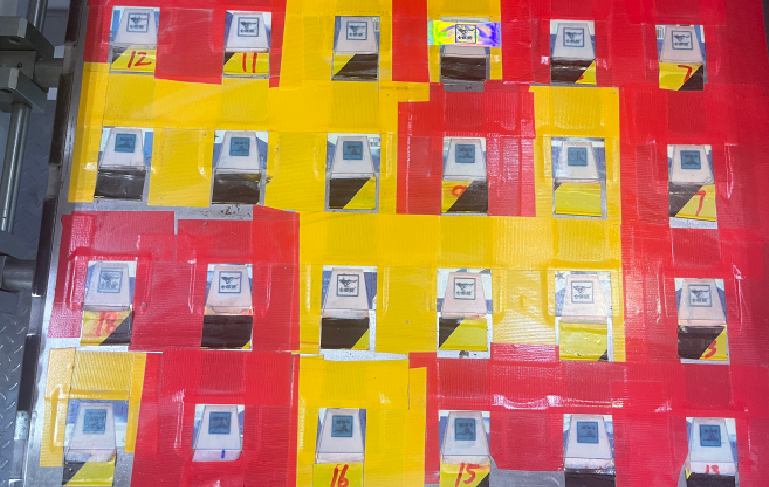
Figure 9 is a schematic diagram showing the overall installation of the embedded rapid compensation 3D stamping process pressure device.
In addition, in actual use of the device, because the pressure is stable and the pressure adjustment time is reduced, the temperature changes caused by downtime are minimized, and the amount of defective stamped products is significantly reduced, increasing the yield. The annual proportion of defective stamping on the small packs of "Seven Wolves (Blue)" cigarettes dropped from a peak of 24.87% to 4.75% in 2025, effectively lowering the defect rate in stamping.
These practices show that the embedded rapid compensation 3D stamping process pressure device has advantages such as a reasonable structure, low manufacturing cost, and easy installation and operation. This device can also be applied in other scenarios and has certain promotion value in stamping processes.