


Years of real-world testing reveal that the key to aluminum foil inkjet printing boils down to two issues
In traditional printing processes, roll-type aluminum foil materials are often flexographized, while single-sheet aluminum foil is offset printing. A relatively mature process system has now been established to suit the special printing suitability of aluminum foil materials. For example, to enhance color vibrancy and improve adhesion between ink and aluminum foil materials, the industry commonly uses specialized inks mainly composed of polyphthalamine or vinyl chloride vinyl acetate copolymerization resins.
With the growing demand for personalized market and the rapidly changing market environment, the proportion of orders for small-batch, multi-variety aluminum foil printing orders continues to rise. Inkjet printing, with its core advantages of small batches and personalization, has become an important direction to meet this demand. However, how to ensure high-quality printing in aluminum foil printing and empower enterprises has become an urgent issue for the industry.
The needs and pain points of inkjet printing in aluminum foil material applications
Aluminum foil differs significantly from traditional printing materials such as paper, PVC, PET, BOPP, and others. In inkjet printing processes without dedicated inks, two core issues are usually encountered:
First, aluminum foil has high tensile strength, is almost non-stretchable, has low tear strength, and has a smooth surface. During roll-to-roll printing, issues such as slipping and misalignment can easily occur, potentially scratching the printhead.
Second, the surface energy of aluminum foil materials is relatively low, resulting in poor adhesion after the ink layer dries on the printed surface, making ink dropping more likely.
Based on these issues, industrial-grade inkjet printing equipment on the market rarely attempts aluminum foil printing. The author has been engaged in research on digital inkjet printing solutions for many years and now shares relevant practical experience with industry peers to provide references for industry applications.
Pain Points Solution for Aluminum Foil Inkjet Printing
01
Solves issues such as paper slippage, misalignment, and nozzle scratches
Given the smooth surface and low tensile properties of aluminum foil, we need to set the tension during production to a certain extent without wrinkling or damage, thereby preventing material slippage on the paper guide roller and preventing deviation caused by unstable material transmission. At the same time, appropriately increasing the tension can also improve material warpage to some extent and reduce the probability of the printhead being scratched.
It should be noted that there is no unified standard for tension settings-different equipment manufacturers use different servo drive systems and tension optimization methods. It is recommended to increase tension as much as possible in actual production, while ensuring the material does not slip.
02
Solves issues of poor ink adhesion and ink dropping
To solve the problem of ink adhesion, it is first necessary to understand the core impact of surface tension: Currently, the surface tension of inkjet printing inks on the market is generally around 38 dyn/cm³. Only when the surface tension of the printing material exceeds the ink surface tension can good wetting be achieved and ink shedding avoided. However, untreated aluminum foil rarely achieves surface tension above 38 dyn/cm³; Moreover, the surface of aluminum foil lacks pores, so ink cannot penetrate inside, creating an "anchoring effect." Even after ink transfer and drying, ink loss is still prone to occur.
To address this issue, we often use corona treatment or pre-coating processes to solve it. The specific practice is as follows.
(1) Corona treatment process
The principle of corona treatment is to apply a high-frequency voltage between the insulating electrode and the grounded dielectric drum, breaking down the air between the two electrodes and plasmaizing it; When these plasma particles interact with the surface of the aluminum foil, they can open chemical bonds on the material's surface, form free radicals, accelerate surface activation, thereby improving the surface energy and wettability of the aluminum foil, and ultimately enhancing the adhesion strength between the ink and the aluminum foil surface.
In actual production, a corona device can be installed on inkjet printing equipment to achieve online corona treatment, but the corona power must be determined through testing. Taking a corona device with a power of 2kW as an example, the conventional test parameters are 30%~50% power ratio; If about 50% power is used for corona treatment but ink concentration and ink loss still occur, it indicates that corona treatment cannot improve printing results, so there is no need to further test other power ratios and can be switched to pre-coating process optimization.
Tests have shown that aluminum foil, as a conductive material, can significantly increase its surface energy through corona treatment, but there is still room for optimization (see Figure 1 for comparison of results).
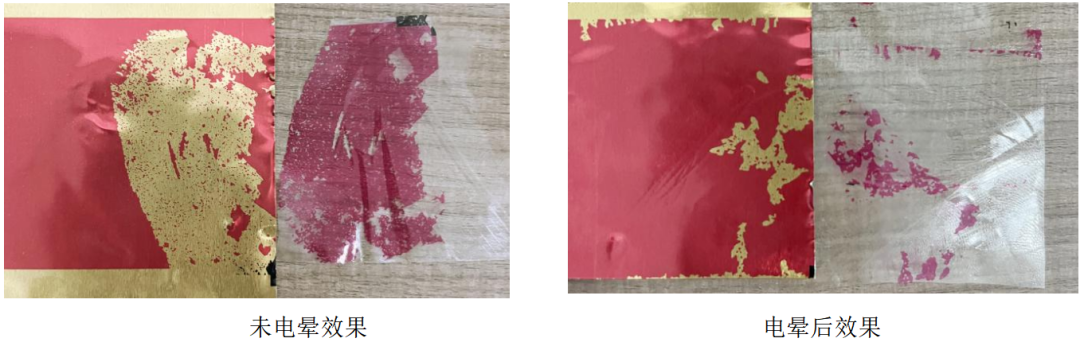 Figure 1 Comparison of Corona Effects
(2) Pre-Coating Process
After long-term systematic testing, the author found that the pre-coating process can significantly improve ink adhesion. However, three key issues need special attention: the choice of screen roller mesh (to control pre-coating amount), the pre-coating method (inline/offline), and the compatibility of the pre-coating solution with the ink. These all need to be determined through practical testing.
The choice of screen roller can refer to the following standards: for conventional materials, 600–1000 line screen rollers with an ink carrying capacity of about 3.95 bcm³ are commonly used; for special materials like aluminum foil, tests suggest using a screen roller of around 800 lines. The coating doesn't need to be too thick to meet ink adhesion requirements.
Pre-coating methods are divided into offline and inline: offline pre-coating means first applying pre-coating to the aluminum foil using the flexo press, and then running the pre-coated foil through the inkjet press for printing; inline pre-coating means integrating a flexo unit into the inkjet press, allowing pre-coating and inkjet printing to be done in one pass, offering greater adjustment flexibility. The author recommends using inline pre-coating for aluminum foil inkjet printing.
Selecting the pre-coating solution requires considering two aspects: first, the compatibility of the pre-coating solution with aluminum foil, which can be addressed by choosing a conventional flexo pre-coating solution suitable for the type of foil; second, the compatibility with digital ink, which must be verified through machine testing based on the digital ink brand used, after ensuring foil compatibility.
Pre-coating thickness significantly affects ink adhesion. As shown in Figure 2, the left image shows a result with a too-thick pre-coating, which still experienced ink loss during scratching; the right image shows a properly applied pre-coating thickness, where even with obvious scratches, no ink loss occurred.
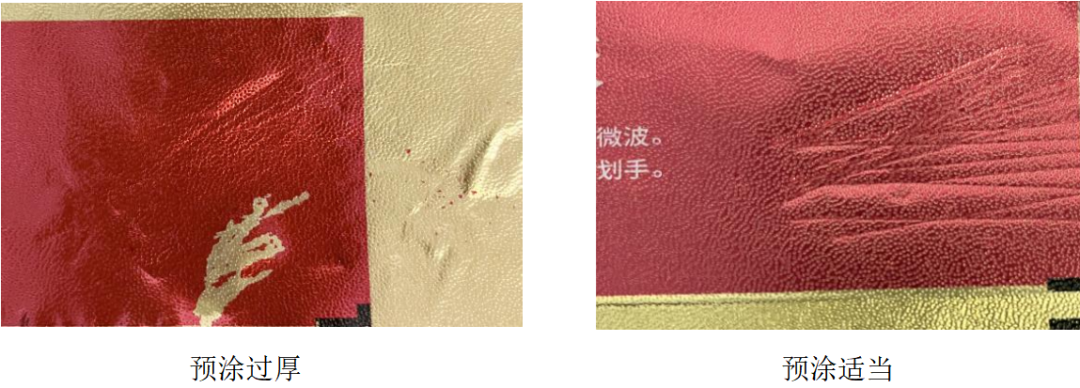 Figure 2 The Effect of Coating Thickness on Ink Adhesion
Thanks to its unique performance advantages, aluminum foil is being used more and more in the printing and packaging field. Small batches, personalized orders, and short delivery times have become the core demand trends in the upstream printing market. This requires professionals in digital printing to further optimize the printability of aluminum foil and improve related solutions. I will continue to explore the inkjet printing process for aluminum foil in depth and keep sharing experiences with peers to help the industry improve together.