


The defect rate dropped by about 60%, and there's actually a new solution for cigarette pack overprinting!
In cigarette pack production, not only is superb craftsmanship required, but the quality standards are also very strict. Among them, overprint accuracy is one of the key indicators of printing quality. Currently, domestic cigarette pack gravure printing generally uses a photoelectric scanning automatic registration system (hereinafter referred to as the 'traditional tracking system'), which works by scanning the edges of printed patterns or specific cross marks to feedback signals that adjust the cylinder phase.
However, in actual production involving multiple brands, small batches, and quick plate changes, there are still many pain points: different brands have significantly different pack designs, overprint color sequences, cylinder circumferences, and layout designs all vary; widely used substrates like transfer silver cardboard and holographic cardboard have complex surface characteristics, such as high reflectivity or uneven aluminum coating. These factors often make it difficult for traditional tracking systems to achieve stable tracking, causing cyclical or random registration deviations. In severe cases, registration errors can reach ±0.15mm or more (as shown by the registration mark arrows in Figure 1), far exceeding internal standards (usually ≤±0.10mm), resulting in a large amount of waste and downtime for adjustments. To address this problem, there is an urgent need for a stable overprint reference solution that isn't affected by plate patterns or substrate surface characteristics.
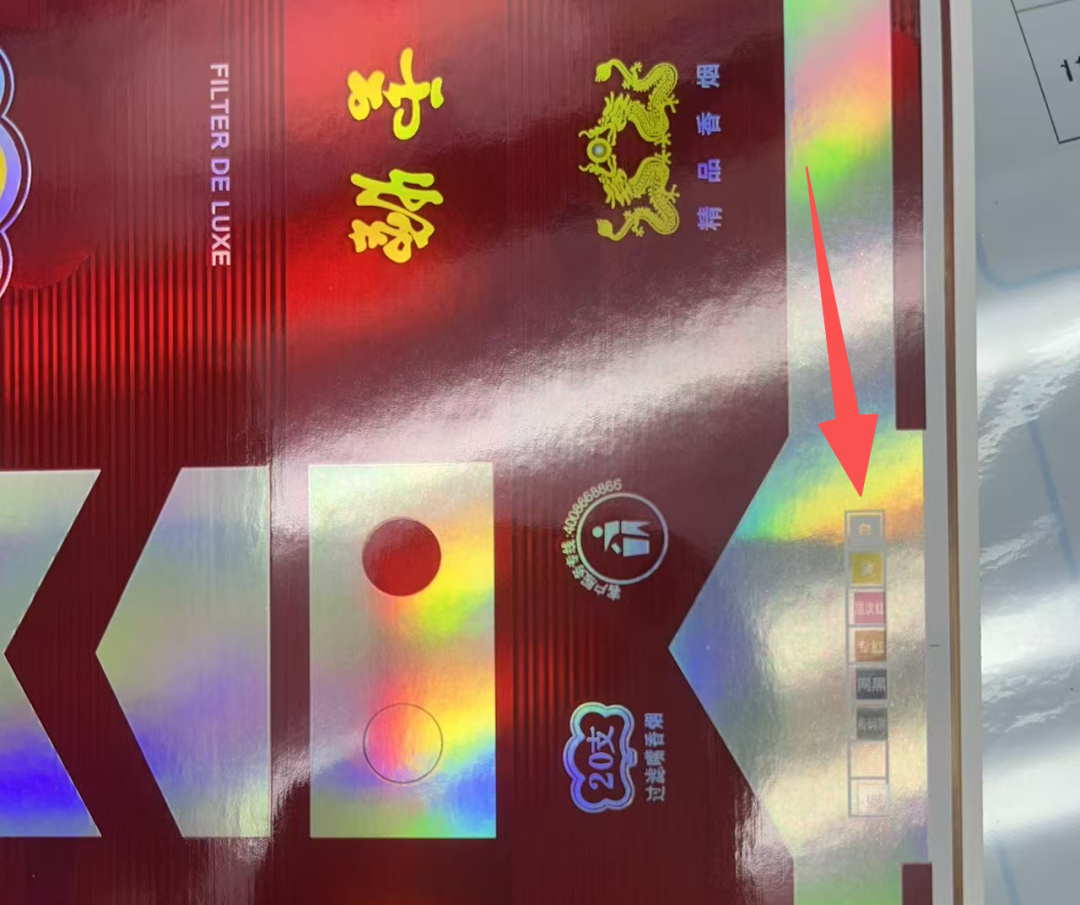
Figure 1: Printed Product Before Improvement
Analysis of Key Factors Affecting Register Stability
Misregistration is a systemic problem rooted in the disruption of dynamic balance during the printing process. The following three factors are especially critical.
01/ Impact of Printing Tension Fluctuations on Transfer Silver Board
Tension is the "lifeline" of flexographic printing presses and has a decisive impact on registration.
(1) Material Characteristics: Transfer silver board is stiff and highly moisture-absorbent, and it may slightly expand or contract during drying. If the tension settings for unwinding, rewinding, or between press units are improper or fluctuate, it directly causes changes in the paper path length, resulting in longitudinal misregistration.
(2) Tension Matching Requirements: The tension gradient between printing units must be accurately matched. Too little tension makes the paper slack, prone to lateral drifting; too much tension stretches the paper, causing shrinkage after drying, which also leads to misregistration. For multi-color flexographic printing, the response speed and stability of the tension system are crucial.
02/ Impact of Plate Cylinder Precision and Condition
The printing plate cylinder is the carrier of image transfer, and its quality directly affects register accuracy.
(1) Radial Runout and Dynamic Balance: For new or restored plates, if radial runout exceeds limits (usually ≤0.02mm) or the dynamic balance is poor, operating at 250 m/min will produce periodic vibrations, directly translating into periodic registration errors.
(2) Cylinder Installation and Thermal Expansion: Misaligned installation, worn keyways, or uneven thermal expansion from frictional heat during continuous printing can change the effective circumference of the plate cylinder, affecting longitudinal register accuracy, with these impacts accumulating over time.
03/ Impact of Mark Quality and Recognition
Traditional marks are printed directly on the substrate and act as the "eyes" of the register system.
(1) Print Quality: On silver board, ink adhesion and drying speed affect mark edge clarity. If the mark is blurry, frayed, or dirty, the photoelectric sensor cannot consistently detect it, causing frequent corrections or misoperations.
(2) Position Interference: If the mark is placed in a complex or highly reflective area of the image, background interference significantly lowers the signal-to-noise ratio, resulting in unstable tracking.
"Roll-plate Registration" Innovative Solution
The core idea of this solution is to move the registration reference mark, the "mark," from the substrate to a separate, high-precision mechanical disk, as shown in Figure 2, completely avoiding interference from the substrate surface or printed designs.
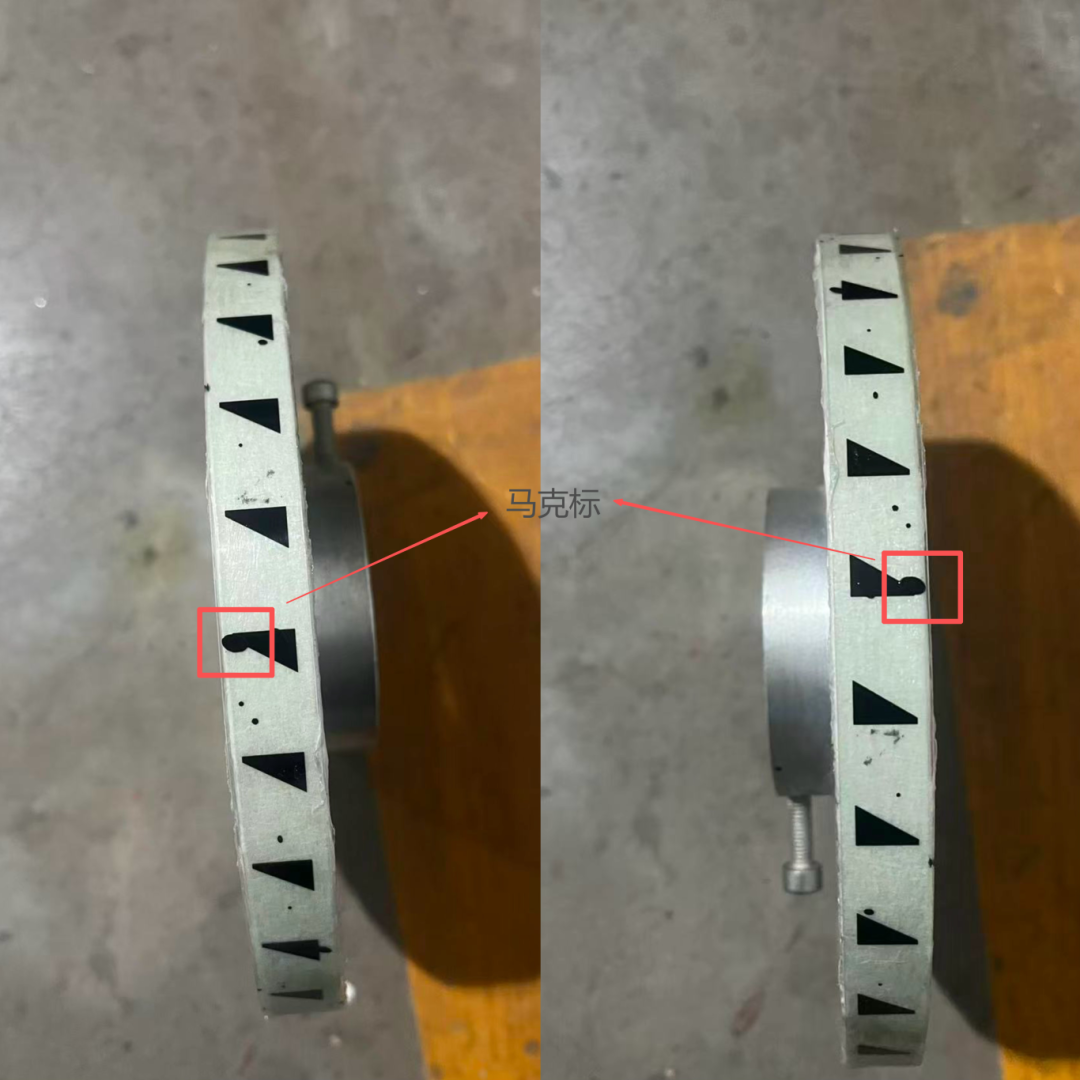
Figure 2 Mechanical Disc Markers
01/ System Composition
(1) Custom Registration Disc: The disc is precision-machined from high-rigidity, low thermal-expansion aluminum alloy or composite materials, usually with a diameter of 150–200mm (customizable according to machine space) and a thickness of 15–20mm. The end-face runout should be ≤0.01mm, and the surface is matte-finished.
(2) High-Precision Markers: Specialized reflective or transmissive markers with high contrast and sharp edges are used.
(3) Mounting Base: A sturdy fixture is designed to mount the registration disc on the stationary part of the printing unit's plate cylinder (near the drive side), ensuring no direct mechanical linkage with the printing roller system while keeping the position fixed.
02/ Specific Operation Steps
(1) Step One: Installation and Calibration
① Securely install the registration disc near the frame of the first color group (reference color group) using a customized fixture, making sure the disc plane is parallel to the plate cylinder axis.
② Mark the disc circumference at precise positions, usually 0°, 90°, 180°, and 270°, and attach high-precision markers. Use a micrometer to calibrate the disc's end-face and radial runout, ensuring total runout is <0.02mm.
③ Adjust the optical sensors for each color group or add dedicated sensors, so that they can stably and clearly scan the markers on the disc, rather than markings on the paper.
(2) Step Two: System Parameter Settings
① Tension Parameters (example: a 10-color gravure press from a certain brand, transferring 125g/m² silver-coated paper): Unwinding tension set to 180–220N; feeding tension set to 200–240N; inter-color group tension increment set to 8–12N; rewinding tension set to 260–300N. Adjust slightly based on specific paper and speed, aiming for smooth, vibration-free paper feed.
② Registration System Parameters: Switch scanning mode to 'Disc' mode; adjust the tolerance window according to the precision of the disc markers for higher sensitivity; set response speed to medium-high to avoid over-sensitivity causing oscillation.
(3) Step Three: Closed-Loop Operation
After power-on, the registration system continuously tracks the fixed markers on the disc. Since the disc position is absolutely fixed, any phase changes of the plate cylinder relative to the machine reference caused by vibration or thermal expansion are detected in real-time, and the system drives the cylinder phase motor for compensation, forming a stable closed-loop control system based on the disc as the absolute reference.
Application Effect and Parameter Comparison
Since implementing this method on a main model, the results have been very impressive.
01/ Significant Improvement in Registration Accuracy
Traditional methods have large registration error fluctuations, especially during roll changes and acceleration, with errors ranging from ±0.12mm to ±0.18mm. With disc registration, accuracy remains stable within ±0.08mm long-term, and can reach ±0.05mm at best, as shown in Figure 3, exceeding industry high-end standards.
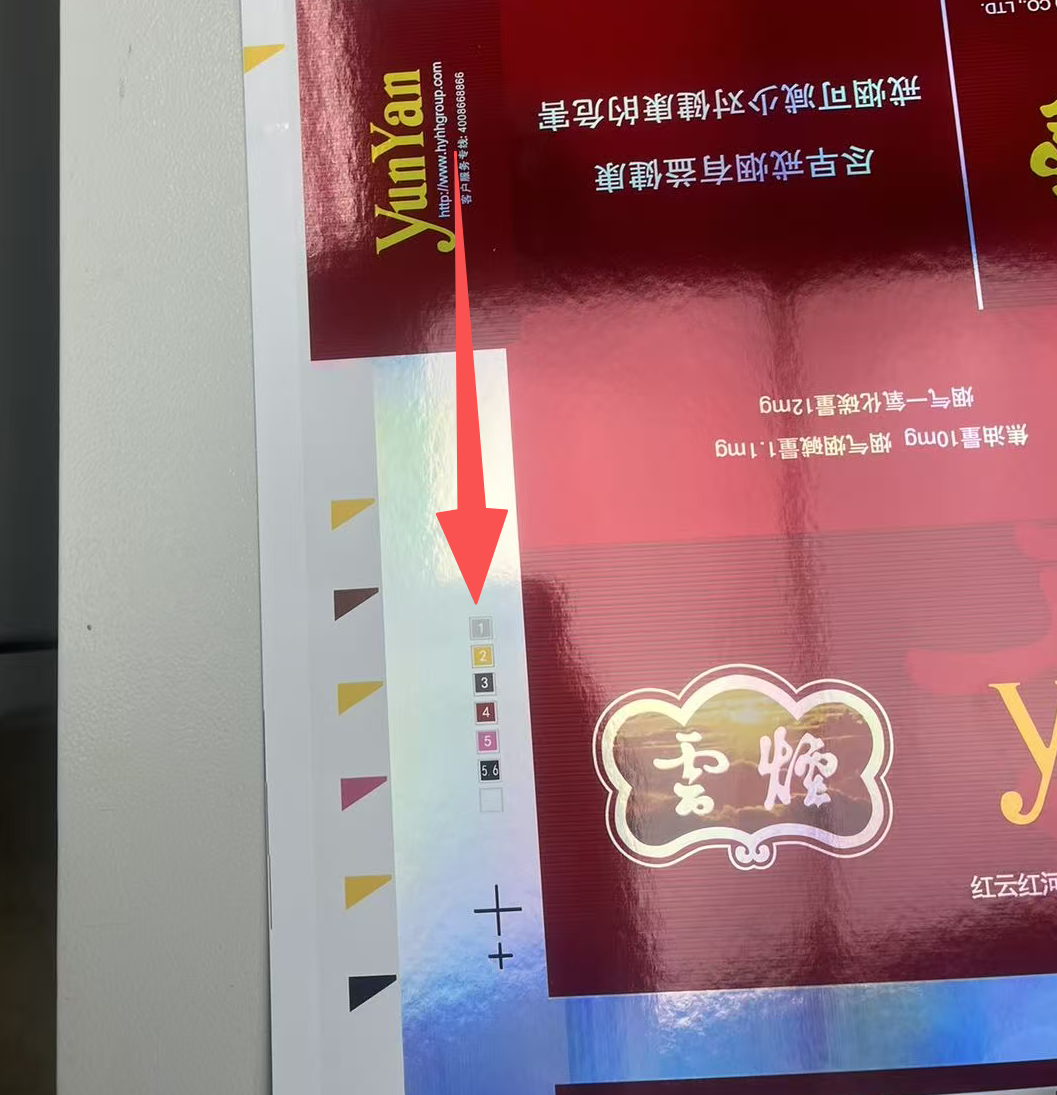
Figure 3 Products printed using register discs
02/ Enhanced Stability and Adaptability
Completely solves tracking loss issues caused by reflective silver paper, barcodes, and other patterns; highly adaptable to printing rollers of different brands and circumferences, with the average initial registration adjustment time after plate changes reduced by about 40%.
03/ Production Efficiency and Cost-effectiveness
Defect rate due to registration issues drops by about 60%; reduces the consumption of extra paper, ink, and other materials caused by registration adjustments; noticeably improves effective equipment operation rate.
For the problem of misregistration in cigarette package gravure printing caused by material and roller variations, the proposed "disc-following registration" solution shifts the registration reference from the changing substrate to a fixed high-precision mechanical disc, effectively isolating the main interference factors at the source. By finely controlling tension, ensuring roller quality, and using an independent disc to provide stable signals, it transforms the registration system from "passive following" to "actively stable." Practical data shows that this solution can control registration accuracy to a high level of ±0.08mm, significantly improving production stability and economic benefits, and is valuable for widespread application in high-end packaging printing. In the future, further exploration can integrate disc-following with roller temperature monitoring and online tension feedback systems to achieve smarter pre-compensation control.