


Yield rate over 99.5%, a quick guide to solving the digital efficiency UV varnish brushing issue
With the digital transformation and upgrading of the packaging and printing industry, digital efficiency-enhancing processes, with advantages like no plate-making, fast response, adaptability for small-batch multi-category production, and high graphic reproduction accuracy, are widely used in the production of adhesive labels for high-end fast-moving consumer goods like alcohol and pharmaceuticals. UV inkjet varnishing, as a key post-printing finishing process for labels, can effectively enhance surface gloss, scratch and wear resistance, and three-dimensional texture, making it a core technique for increasing the added value of label products.
In actual mass production, the stringing issue in digital UV varnish is a common and recurring defect, often occurring in large solid coating areas, gradient transition zones, and along the edges of fine lines and small text graphics. The problem mainly manifests as thin trailing strings, horizontal streaks, frayed edges, and intermittent stringing. Mild cases affect the visual consistency of entire batches, while severe cases can lead to batch scrap, causing material waste and production delays.
Currently, domestic research in the printing industry mostly focuses on screen printing and offset UV varnish issues. Systematic studies on the stringing mechanism, causal coupling, and standardized rectification processes specifically for digital efficiency-enhancing varnish are relatively lacking. Workshop production largely relies on operators' experience for adjustments, lacking theoretical support and standardized procedures, resulting in a high recurrence rate and poor process stability.
Therefore, this paper, based on digital efficiency-enhancing processes and UV curing principles, combined with a large amount of on-site experimental data, systematically analyzes the formation mechanisms and multi-factor patterns of the stringing problem, and develops a full-chain solution from emergency handling, process optimization, equipment correction to source-level prevention, providing a technical basis for improving quality, reducing costs, and standardizing production of digital efficiency-enhancing processes.
UV Varnish Stringing Issue
Typical Forms and Causes
01
Typical Forms
Through long-term on-site tracking and statistics, there are three typical forms of digital UV varnish stringing issues, each corresponding to different causes.
(1) Edge Stringing Type: Concentrated at the edges of graphic contours and the ends of gradients, appearing as fine intermittent trailing strings, mainly caused by incomplete varnish flow interruption and delayed leveling.
(2) Full-page Fine Line Type: Irregular fine streaks distributed across the entire page, with uneven gloss, usually caused by mismatched varnish viscosity, curing parameters, and production speed, as shown in Figure 1.
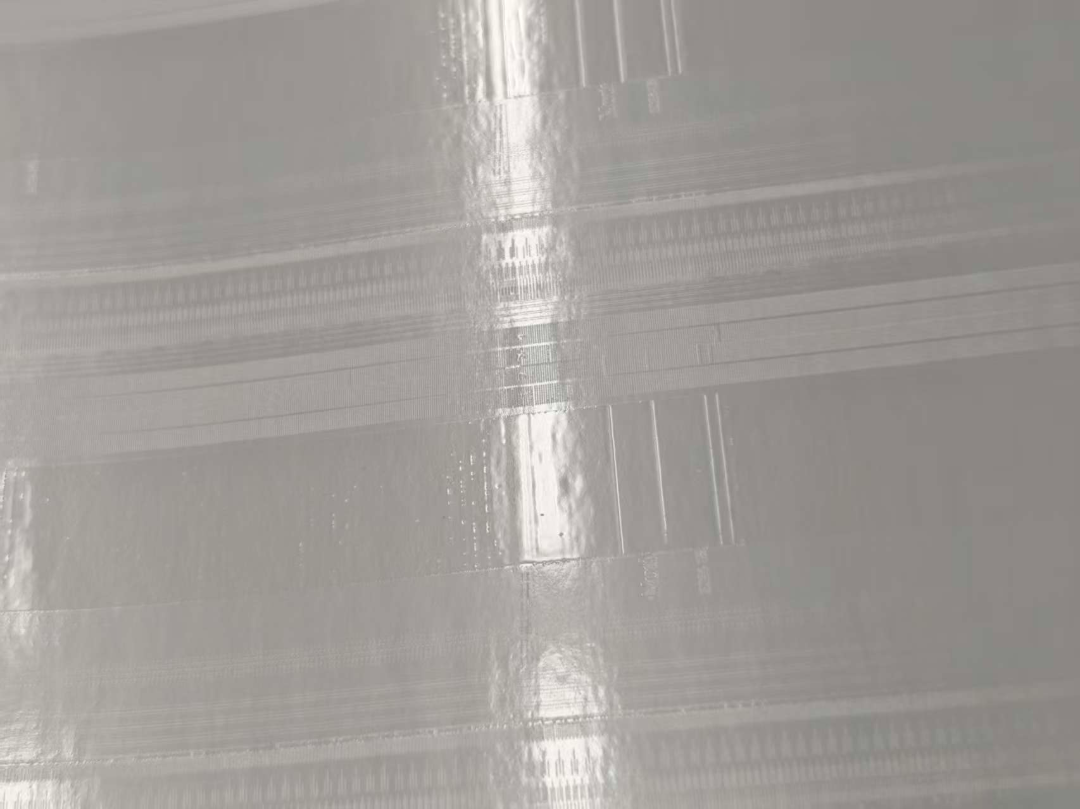
Figure 1 Full-page fine texture type
(3) Regular coarse brushed type: Thick brushing and local oil accumulation appear at fixed intervals, which is a structural issue caused by equipment precision or oil supply system abnormalities, as shown in Figure 2.
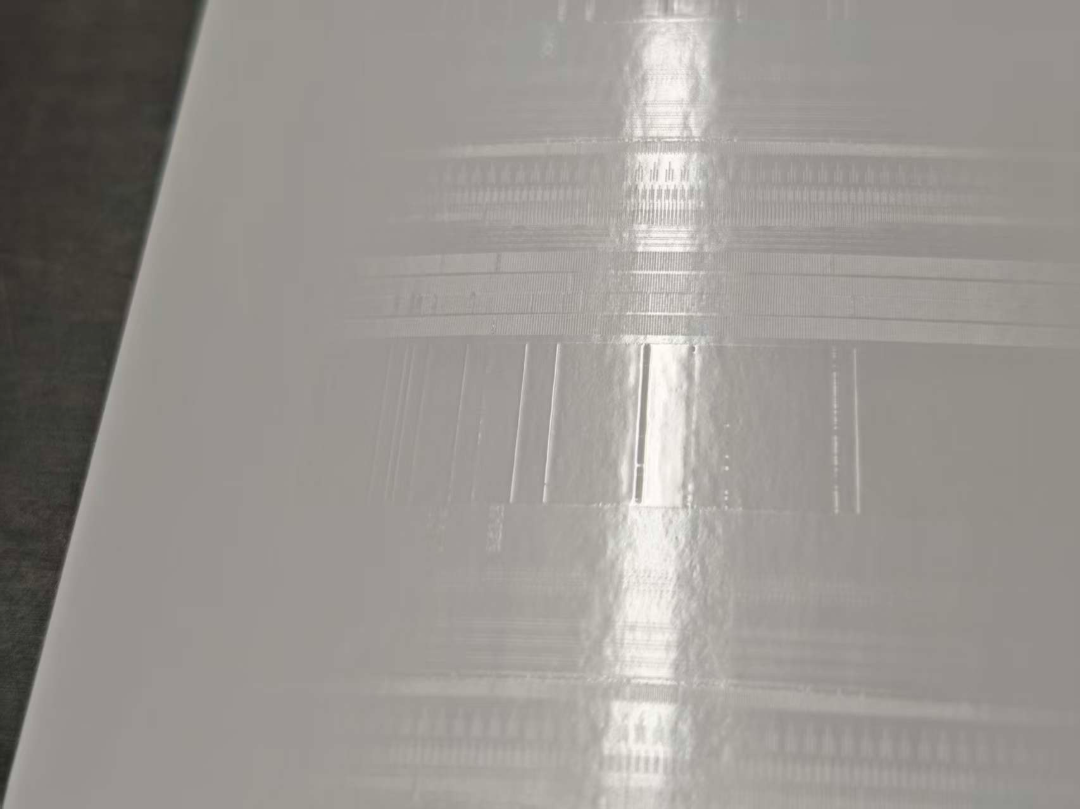 Figure 2: Regular rough drawing type
02
Reasons for molding
The UV inkjet coating molding process includes three consecutive stages: "inkjet liquid - substrate wetting and leveling - UV UV curing and setting." The fundamental cause of the brushing problem can be summarized as follows: before the varnish is fully wetted and leveled and the interface tension balanced, external interference such as mechanical pulling, rapid curing, and physical property instability causes the liquid oil film to undergo non-uniform plastic deformation and is instantly fixed and cured by UV light, ultimately forming irreversible filament-like defects.
In an ideal molding state, varnish rapidly spreads on the substrate surface, with balanced tension and leveling, then is moderately UV-crosslinked and cured to form a dense and uniform varnish film layer. When any parameter of material, equipment, process, or environment is imbalanced, it disrupts the "inkjet-leveling-curing" balance, triggering issues such as drawing strings.
Multidimensional cause analysis
01
Material factors
The rheological characteristics and purity of digital UV varnish drawing problems are fundamental conditions determining the quality of oil film forming.
(1) Excessive viscosity and degraded leveling performance: Digital UV varnish is highly sensitive to ambient temperature. Factors such as low-temperature conditions, solvent evaporation after long open caps, and high batch solid content all increase fluid viscosity and surface tension, leading to reduced spreading speed and extended leveling time. Under high-speed material discharge conditions, pulling and dragging issues are very likely.
(2) Material selection mismatch: Using mixed screen-printed varnish or ordinary coated varnish instead of digital efficiency enhancement specialized varnish can cause issues such as unsmooth liquid discharge, poor flow interruption, and severe wire slag, making it unsuitable for micro-piezoelectric inkjet logic.
(3) Insufficient purity and stability: varnish settles and forms a crum, impurities mix, stirring and foaming, and inadequate filtration can cause intermittent ink output and uneven liquid output from the printhead, with alternating local oil accumulation and deficiency, resulting in filamentous texture problems.
02
Equipment factors
The stability of the equipment's oil supply, injection, transmission, and curing systems directly determines the quality of the coating.
(1) Abnormal nozzle operating conditions: Slight clogging of the nozzle, dry accumulation of residual oil in the nozzle, wear and deformation of the nozzle, leading to issues such as angled spraying, interrupted spraying, and uneven liquid discharge, which can lead to local excessive oil accumulation, resulting in stringing and tailing.
(2) Pressure fluctuations in the fuel supply system: Unstable negative pressure/air pressure of the secondary cartridge, blocked pipelines, and aging filters can cause large pulsations in the fuel supply, fluctuating oil output, forming regular striped brushing.
(3) Unstable feeding transmission: Uneven pressure on the traction rollers, fluctuations in tension, and paper feed shaking can cause uncured soft oil films to be mechanically sheared and pulled, resulting in burrs and stringing.
(4) Abnormal UV curing parameters: excessive curing power or rapid curing can cause the oil film to set before fully leveling; Aging of the lamp tube and insufficient energy can cause incomplete surface curing, causing rewinding friction and secondary dragging issues.
03
Process parameter factors
Mismatch of process parameters is the main trigger for sudden wire drawing in mass production.
(1) Printing speed too fast: The machine speed exceeds the varnish leveling response range, resulting in insufficient leveling time, and the oil film is not smooth, causing dragging lines to form as it moves with the substrate.
(2) Unreasonable ink output and overprinting: Excessive ink output in a single channel and stacking of multiple layers can cause excessive oil film thickness and imbalanced edge tension, resulting in filamentous patterns during natural leveling.
(3) Bidirectional printing alignment deviation: Overlapping and misaligned back-and-forth spraying can cause regular horizontal brushed stripes, which are commonly seen in the same batch.
04
Environmental factors
Workshop temperature, humidity, and cleanliness have a significant impact on the rheology of varnish and forming performance, with constant temperature and humidity in the workshop shown in Figure 3.
(1) When the ambient temperature is below 18°C, the viscosity of the varnish increases significantly.
(2) When humidity is too low (relative humidity <40%), it causes rapid crusting on the surface of the varnish, inconsistent surface and inner leveling, and dry fine lines.
(3) Airborne dust adhering to uncured oil film can disrupt surface flatness and trigger fine drawing defects.
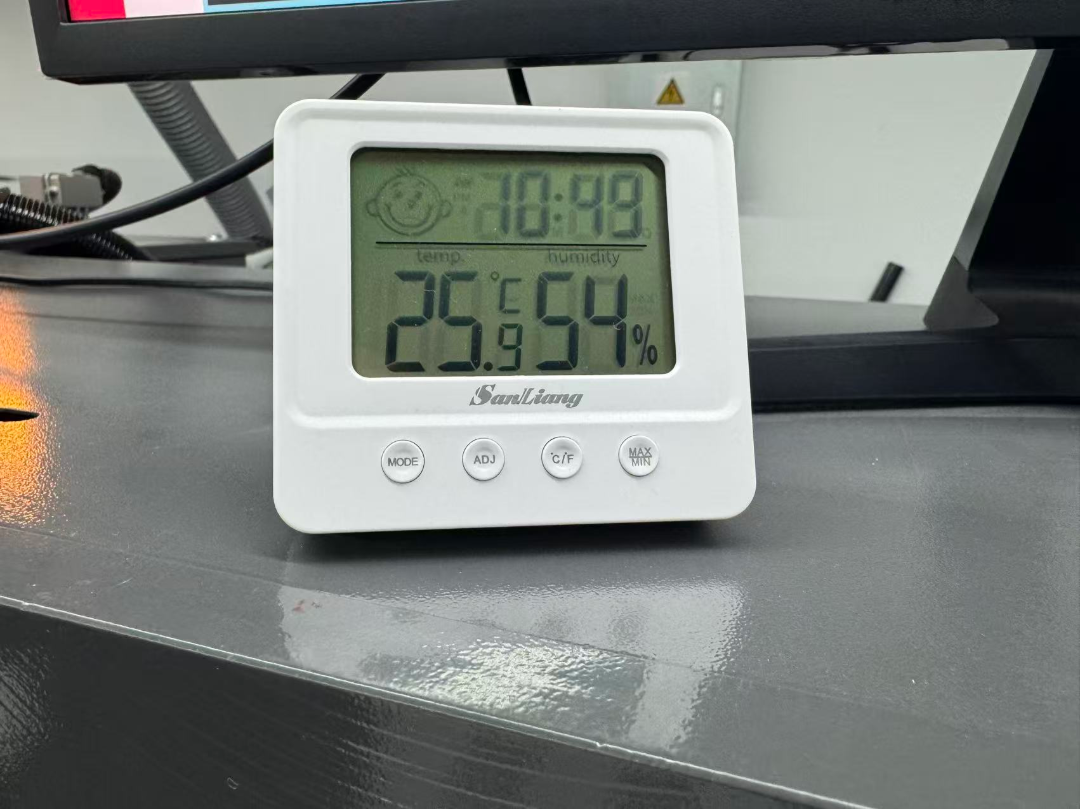 Figure 3: Constant temperature and humidity in the workshop
Tiered optimization technical solutions and implementation processes
By combining the severity of the problem with production continuity requirements, a four-level closed-loop handling system is established, enabling tiered management of digital UV varnish wire drawing issues through non-stop emergency response, batch rectification, hardware eradication, and long-term prevention.
01
Level 1 emergency response
Suitable for sudden slight brushing and occasional tailing at the edges during mass production:
(1) Reduce printing operating speed by 20%~30%, extend oil film leveling time, and eliminate mechanical dragline;
(2) Moderately reduce UV curing power by 10%~15%, slow down the curing pace, and ensure that varnish leveling is prioritized and curing is post-processed;
(3) Perform flash spraying and dust-free surface cleaning to eliminate minor clogging and residual oil buildup.
02
Secondary process optimization
Addressing issues such as uniform fine lines and persistent edge brushing throughout the entire panel:
(1) Precise viscosity control: Standard working environment of 22~25°C, control varnish viscosity at 20~25s (apply 4 cups). High-viscosity materials use micro-blended special UV thinner for stirring, then let it sit for defoaming and filter to 100 mesh;
(2) Precise parameter matching: Reduce single-channel ink output by 5%~10%, optimize the number of overprinting layers, and recalibrate bidirectional printing alignment accuracy;
(3) Stabilizing feeding system: Corrects pressure balance between front and rear traction rollers, fine-tunes tension parameters, and prevents substrate shaking or displacement.
03
Level 3 hardware maintenance
To address recurring issues such as fixed stripes and heavy brushing:
(1) Replace the precision filter, clean the oil supply lines and auxiliary ink chamber, and thoroughly replace the varnish;
(2) Perform deep negative pressure cleaning of the nozzles, repair blocked nozzles and oblique spray issues, and promptly replace worn nozzles;
(3) Check the energy and distance of UV lamps, replace aging tubes, and repair the feeding drive belt and motor stability.
04
Four-level source control
(1) Standardized material management: dedicated materials and dedicated machines, strictly prohibited from mixing across categories; Materials should be stored in a sealed and protected manner;
(2) Standardized environmental control: workshop constant temperature 20~26°C, constant humidity 50%~65%, preheating the lurenishing system in advance during cold seasons;
(3) Standardized equipment maintenance management: pre-shift inspection and cleaning, post-shift oil sealing maintenance, weekly filter element replacement, and monthly overall machine precision calibration.
Standardized pre-production commissioning procedures
To achieve process reproducibility and stable quality, standardized pre-production commissioning procedures should be established:
(1) Material pretreatment: stirring, settling, defoaming, filtering to ensure viscosity and cleanliness meet standards;
(2) Equipment pre-inspection: inspection of sprinkler heads, rubber rollers, optical paths, and oil supply system cleaning;
(3) Low-speed test printing: Print test ladder strips to observe oil uniformity, leveling status, and curing effect;
(4) Parameter fine-tuning: Matching speed, ink amount, and curing power to eliminate poor leveling and drawing;
(5) Batch release: Trial printing is free of brushing, no orange peel, and uniform gloss before mass production.
Analysis of application effects and benefits
This optimization plan was implemented on multiple digital efficiency label production lines, with significant comparison of quality data before and after rectification. Before implementing the graded optimization system, the drawing defect rate was 8%~15%, with high rework frequency and relying entirely on manual experience for process debugging; After implementing the graded optimization system, the issue of UV polish drawing was basically eliminated, and the mass production yield rate remained stable above 99.5%.
This technical solution does not require high equipment upgrades. Through mechanism guidance, standardized parameters, and standardized processes, it effectively reduces material loss, manual rework, and downtime costs, while also reducing dependence on personnel experience, achieving stable processes, controllable quality, and efficient production, fully meeting high-end label appearance acceptance standards.
The digital UV varnish brushing problem is a comprehensive process problem caused by the coupling of material rheological characteristics, equipment operating accuracy, process parameter matching, and environmental working conditions. Its core contradiction is the dynamic imbalance between the varnish leveling timing sequence and mechanical feeding and UV curing rhythms. This paper constructs a practical and replicable governance process system through problem form classification, in-depth mechanism analysis, and layered experimental optimization. Through pre-production standardized debugging, precise in-production parameter matching, and normalized post-production maintenance, the persistent drawing problems in digital efficiency enhancement processes can be thoroughly resolved, significantly improving label printing appearance quality and mass production stability, and providing reference for process upgrades, quality control, cost reduction, and efficiency improvement for similar digital printing enterprises.